Direct Factory OEM/ODM Wholesale Supply & Retail-Ready Packaging Solutions
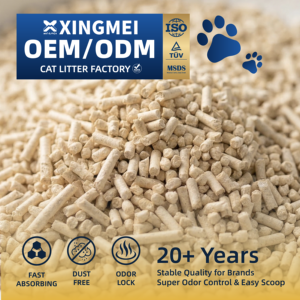
Bentonite, an absorbent aluminum phyllosilicate clay consisting primarily of montmorillonite, serves as the foundational backbone for dozens of multi-billion-dollar global industries. From civil engineering drilling fluids, foundry sand bonding, and metallurgy pelletizing to agricultural soil conditioning, water purification, and premium pet hygiene products, raw bentonite clay possesses unique colloidal and rheological properties unmatched by synthetic alternatives. As the global demand for sustainable, non-toxic, and high-performance mineral solutions accelerates, China has established itself as the world's primary engine for bentonite extraction, purification, and advanced OEM manufacturing.
Partnering directly with an enterprise-grade China Wholesale Raw Bentonite Manufacturer & Factory offers international importers, brand owners, industrial repackers, and commercial distributors an unparalleled competitive advantage. Vertically integrated mining operations—combining raw ore extraction, high-precision solar and thermal drying yards, automated crushing mills, cyclone de-dusting passes, and automated multi-format packaging lines—allow for absolute quality control from mine bench to shipping pallet. By mitigating third-party supply chain intermediaries, direct factory partnerships ensure consistent cation exchange capacity (CEC), predictable moisture retention, precise mesh size distribution, and optimized freight logistics.
Not all bentonite reserves are created equal. Natural Sodium Bentonite exhibits extreme swelling capacity (12–15 times its dry volume) and creates high-viscosity thixotropic suspensions, making it the premier choice for fast-clumping pet litters and drilling muds. Calcium Bentonite, while displaying lower natural expansion, features superior adsorption for liquids and organic molecules, making it ideal for bleaching earths, environmental remediation, and multi-cat hygiene formulations. China’s vast geological reserves contain specialized high-purity deposits of both mineral types, allowing tailored activation and sodium-exchange processes.
For technical procurement directors and industrial engineers, evaluating raw bentonite requires rigorous mineralogical verification. High-grade montmorillonite content directly correlates with clump strength, absorption speed, odor encapsulation, and liquid retention under load. Below is the standard technical specification spectrum produced across our primary processing facilities for commercial and industrial buyers:
| Technical Parameter | High-Purity Sodium Bentonite | Activated Calcium Bentonite | Eco-Hybrid Composite Mix |
|---|---|---|---|
| Montmorillonite Content (%) | ≥ 85.0% - 92.0% | ≥ 78.0% - 85.0% | Customized Plant / Clay Blend |
| Water Absorption Capacity | ≥ 350% - 450% | ≥ 220% - 300% | ≥ 400% - 600% |
| Free Swelling Index (mL/2g) | ≥ 24 - 32 mL | ≥ 10 - 16 mL | N/A (Fiber Matrix) |
| Particle Size / Mesh Band | 0.5 - 1.5mm / 1 - 3mm / 2 - 5mm | 200 Mesh / 325 Mesh Powder | 1.5mm - 2.0mm Pellets |
| Moisture Content (%) | ≤ 6.0% - 8.0% | ≤ 10.0% | ≤ 8.5% |
| Dust Content (De-dusted) | ≤ 0.5% (99.5% Dust Free) | Standard Powder Grade | ≤ 0.2% Ultra-Clean |
| Clump Hardness (N/cm²) | ≥ 15 N (Hard Non-Breaking) | ≥ 10 N | ≥ 18 N (Fast-Disintegrating) |
Our internal R&D laboratory conducts X-ray Fluorescence (XRF) and X-ray Diffraction (XRD) analysis on every mining bench lot to guarantee chemical stability. Low iron content (Fe₂O₃ < 2.5%) ensures a visually appealing bright white to light-cream granule hue, which global retail shoppers associate with maximum cleanliness and hygienic quality.
Achieving consistent technical performance in large-scale commercial shipments requires strict adherence to vertical manufacturing protocols. Our modern processing plant in China operates a multi-stage production line designed to maintain raw mineral integrity while maximizing functional utility:
Carefully managed open-pit extraction isolates pure montmorillonite seams, preventing organic contamination and ensuring uniform mineral color.
Mined raw ore undergoes controlled atmospheric weathering and optional sodium-carbonate activation to optimize cation exchange capacity and swell index.
Thermal moisture reduction is executed at monitored temperatures to preserve the crystalline lattice structure of bentonite, preventing thermal degradation.
Crushed granules pass through high-velocity cyclone air separators and fine vibrating sieves to eliminate 99.5% of airborne particulate dust.
Liquid perfumes (baby powder, lavender, lemon, Marseille soap) or odor-locking activated carbon matrix are uniformly sprayed in-line per buyer spec.
Finished goods are packed into custom printed PE bags, woven bags, buckets, or 1.25 MT big bags with automated robotic palletizing and stretch wrapping.
As the global market for industrial minerals and pet care products matures, procurement managers must navigate changing consumer preferences, stringent environmental regulations, and logistics complexities. Key developments shaping global raw bentonite procurement include:
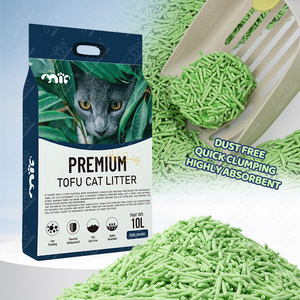
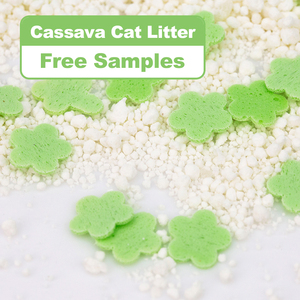
While traditional 100% sodium bentonite remains the global sales volume leader due to its affordability and hard clumping power, retail markets in Europe, North America, and Asia are rapidly adopting hybrid composite litters. By blending premium sodium bentonite with plant-based fibers—such as Tofu (Soybean), Cassava Starches, and Corn Substrates—manufacturers create light-weight, highly absorbent, low-dust, and flushable hybrid products. Our factory specializes in custom formulations, combining bentonite's structural clump density with plant fiber biodegradability.
Regulatory bodies and pet health advocacy groups are increasingly focusing on airborne crystalline silica exposure. Modern global importers require certified sub-0.5% dust metrics. Advanced multi-stage dust extraction systems installed at our factory ensure that every ton of bentonite shipped meets international safety audits, protecting household indoor air quality and pet respiratory health.
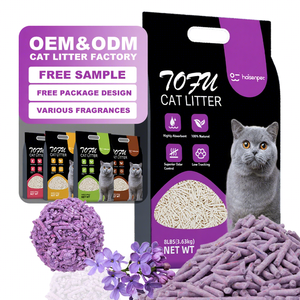
The shift toward direct-to-consumer (DTC) e-commerce brands and supermarket private labels has transformed packaging needs. Procurement is no longer just about buying raw minerals in bulk; it requires turn-key OEM solutions. Our factory provides full structural bag design, flat-bottom quad-seal bags, ergonomic carry handles, vacuum sealing, barcoding, master carton packing, and pallet wrapping tailored for instant Amazon, Walmart, or specialty pet store shelf listing.
Selecting the right manufacturing partner in China is a strategic decision that directly impacts brand reputation, profit margins, and inventory reliability. As a vertically integrated enterprise operating our own mineral reserves and dedicated processing infrastructure, we offer unmatched advantages:
1. Complete Supply Chain Traceability: From the specific mining pit bench to the final shipping container number, every shipment carries a documented paper trail. Batch-to-batch consistency is guaranteed, eliminating the risk of unannounced raw material substitution common among trading intermediaries.
2. Flexible Packaging & Format Options: Whether you require 5-liter retail bags, 10 kg quad-seal handles, durable plastic buckets, or 1,250 kg big bags for local repacking lines, our high-speed automated packaging machinery satisfies all global retail and industrial formats.
3. Rigorous Quality Certification & Compliance: All manufacturing operations strictly comply with ISO 9001:2015 Quality Management Systems and ISO 14001 Environmental Standards. Material Safety Data Sheets (MSDS), REACH registrations, and heavy metal testing reports are provided with every export container.
Launching a new brand or expanding an existing retail product line? Our experienced export engineering team offers complimentary artwork proofing, bag structural design consulting, custom fragrance matching, and trial batch production before full container loading.
Our standard Minimum Order Quantity (MOQ) for full OEM private label customized packaging is 1x20' Container (approx. 20-24 Metric Tons depending on package density). For standard bulk big bag shipments or unprinted stock packaging, smaller trial quantities can be arranged upon request.
Natural white calcium bentonite features an aesthetically clean, bright appearance with low iron content, preferred by premium consumers. When activated or blended properly, it delivers exceptionally hard, fast clumps without leaving dark gray mud marks in litter boxes. Natural sodium bentonite offers inherent high expansion, making it a robust, cost-effective clumping engine.
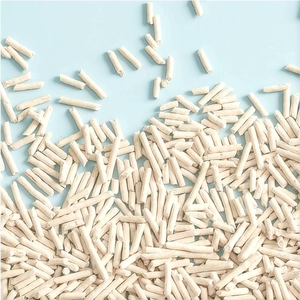
Standard granule size bands include 0.5–1.5 mm (fine fast-clumping), 1.0–3.0 mm (classic benchmark), and 2.0–5.0 mm (coarse low-tracking). Fragrance choices include Unscented, Baby Powder, Lavender, Marseille Soap, Vanilla, Apple, Lemon, and Carbon Odor-Lock. Custom scent dosage and granule sizing can be adjusted during sample trials.
Yes. Every export shipment includes comprehensive Technical Data Sheets (TDS), Safety Data Sheets (SDS), Quality Analysis Certificates (COA), and Certificate of Origin (Form E, CO, etc.) required for smooth customs clearance and retail regulatory compliance in destination seaports.
For repeat orders, standard production lead time is 10–14 days from deposit confirmation. For new private label orders requiring custom bag printing plate creation, the initial lead time is approximately 20–25 days.
Connect directly with our engineering and export team to request technical datasheets, order sample kits, or obtain competitive factory-direct container pricing.
Inquire Now