Export-ready OEM/ODM pet care packaging systems, bio-degradable substrate formulations, and high-performance clumping solutions engineered for multinational brands and retail distributors.
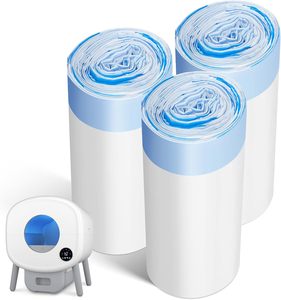
Heavy-duty co-extruded LDPE polymer construction featuring high tensile strength, leakproof thermal seams, and integrated drawstring closure systems for hygienic sanitation management.
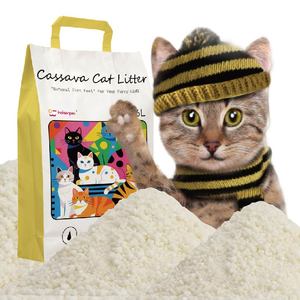
Ultra-absorbent plant-based substrate synthesized from organically farmed cassava starch. Delivers solid aggregation within 1.5 seconds and immediate moisture encapsulation.
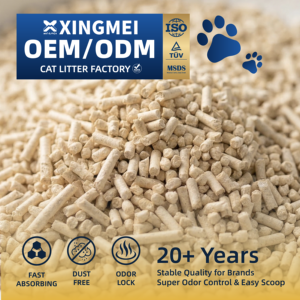
Commercial grade 2.0mm micro-extruded pea fiber tofu litter processed through triple cyclone dust-extraction chambers. Packaged in vacuum-sealed retail block bricks.
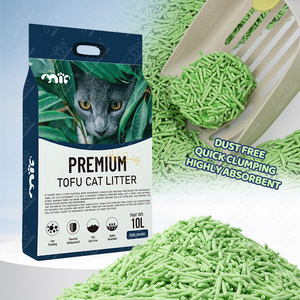
Optimized high-rotation retail formulation delivering rapid capillary action and superior mechanical clump rigidity, built specifically for mass-market supermarket distribution.
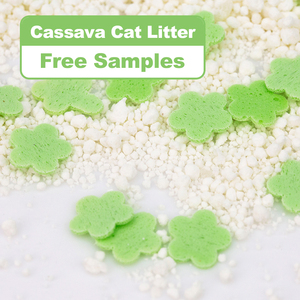
Custom branded cassava substrate enhanced with bio-enzymatic odor-neutralizing complex. Available with customized granule sizing (0.5mm-2.0mm) and bespoke scent infusion.
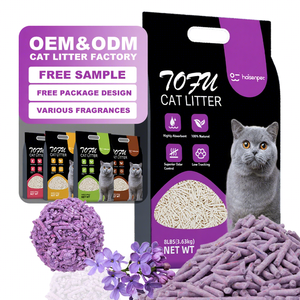
100% water-soluble natural plant fiber substrate engineered for rapid disintegration upon immersion in residential sewage systems without clogging pipes.
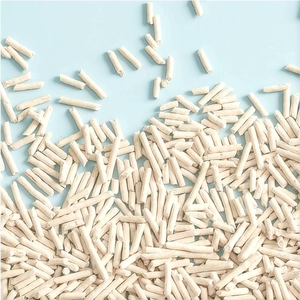
Precision-engineered 2.0mm micro-pellet formulation synthesized from corn meal and pea fiber. Minimizes paw tracking while maintaining ultra-fast hydraulic liquid absorption.
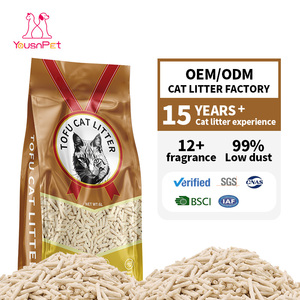
High-density plant matrix specifically developed for multi-cat households. Provides structural clump stability, minimal dusting, and long-lasting nitrogenous odor control.
The global pet supply and bulk packaging export ecosystem is undergoing a fundamental structural transition. Driven by stringent environmental compliance frameworks in the European Union (such as the Packaging and Packaging Waste Regulation - PPWR) and North American ESG disclosure mandates, corporate buyers, supermarket chains, and private-label brand owners are systematically migrating from traditional mineral/synthetic supply chains toward circular eco-friendly materials, bio-degradable polymers, and vertically integrated OEM manufacturing hubs.
As premier Chinese wholesale bulk packaging factories and global exporters, our manufacturing facilities integrate upstream raw material processing (including natural pea fibers, organically sourced cassava starches, and high-purity mineral reserves) with state-of-the-art automated packaging film extrusion, gravure flexographic printing, and vacuum sealing systems. This vertically integrated manufacturing model addresses critical global procurement vulnerabilities: supply chain fragmentation, lot-to-lot performance variances, high shipping volume costs, and regulatory non-compliance.
To assist international procurement directors and brand technical leads in selecting optimal wholesale product lines, the following empirical comparison details key physical metrics across our major plant-based and mineral export formulations:
| Substrate Classification | Primary Raw Material | Hydraulic Absorbency Rate | Clump Shear Strength (N) | Dust Particle Index (<100μm) | Primary Target Retail Market |
|---|---|---|---|---|---|
| Cassava Micro-Granules | Organic Cassava Starch | 450% - 500% by weight | > 18.5 N (Instant) | < 0.2% | Premium Eco Brands, Vet Clinics |
| 2.0mm Micro Tofu Pellets | Pea Fiber & Corn Starch | 300% - 350% by weight | > 15.2 N (Within 3 sec) | < 0.4% | Supermarket Chains, E-Commerce |
| White Bentonite Agglomerates | Natural Calcium Montmorillonite | 250% - 280% by weight | > 22.0 N (Hard Clump) | < 0.5% (Triple-Screened) | Mass Market Retail, Discount Chains |
| Co-Extruded Poly Liners | Virgin LDPE / HDPE Blend | Tensile Yield: >25 MPa | Puncture Force: >48 N | Zero Particle Generation | Sanitation Accessories, OEM Packs |
*Data verified via internal QA laboratory testing under standardized ISO 20200 and ASTM D882 testing protocols.
Analysis of emerging industrial shifts, sustainable material engineering, and intelligent packaging innovations driving the next decade of international trade.
Global regulatory bodies are rapidly phasing out multi-layer non-recyclable plastic laminates. The market is shifting decisively toward Mono-PE (Polyethylene) recyclable structures and compostable PLA/PBAT bio-polymers. Our export packaging lines feature state-of-the-art MDO-PE film integration, maintaining essential oxygen/moisture barrier properties while allowing 100% downstream recycling compliance in European and North American municipal facilities.
Consumer preferences in urban apartment settings have fueled rapid demand for small-diameter pellets (1.5mm–2.0mm micro-tofu and 0.5mm–1.5mm cassava granules). Micro-granules provide vastly superior surface area contact, reducing fluid consumption per usage cycle by up to 30% while dramatically lowering paw tracking on household floors. Advanced die-extrusion technology allows precise geometric uniformity and density control.
Simple scent masking is no longer sufficient for discerning pet owners. Modern sourcing specifications require integrated biochemical odor encapsulation. By co-extruding bio-enzymes, activated bamboo carbon nanoparticles, and natural deodorizing complexes directly into the plant fibers during thermal extrusion, odor-causing ammonia gas is neutralized at the molecular level rather than temporarily fragrance-masked.
Ocean freight cost volatility makes container volume optimization a vital competitive metric. Modern Chinese export factories utilize continuous high-vacuum automated brick-packing machinery. Vacuum packaging reduces shipping cubage by up to 40% compared to loose bags, allowing buyers to maximize unit payload per 40ft High Cube container while providing robust protection against humidity during ocean transit.
Navigating global B2B procurement demands absolute transparency, certified product consistency, and flexible manufacturing capabilities. Our industrial infrastructure is engineered to serve high-volume supermarket chains, regional brand distributors, and e-commerce leaders through a fully integrated OEM/ODM framework.
Direct access to raw plant materials and proprietary white bentonite reserves ensures uninterrupted raw supply, lower baseline cost structures, and tight control over mineral purity and starch grades.
In-house 10-color gravure printing, automatic bag making, quad-seal handle bag extrusion, and corrugated master carton forming eliminate third-party converter margins and production delays.
Every shipment undergoes comprehensive laboratory checks: moisture testing (target <8%), sieve breakdown analysis, dust particle counting, and drop-test packaging validation before container sealing.
Clear, direct technical answers regarding minimum order quantities, private label customization, international shipping compliance, and performance specs.
Connect directly with our engineering and export sales teams to request custom sample kits, obtain technical specification sheets, or receive factory-direct wholesale FOB/CIF price quotations.