Explore high-volume OEM/ODM export products direct from China's leading manufacturing hubs.
Analyzing key structural advantages, production capacity, and supply chain dynamics driving global market demand.
The global pet care industry has undergone a monumental shift toward premiumization, sustainability, and functional hygiene. As multi-cat households expand across North America, Europe, the Middle East, and Asia-Pacific, international importers, supermarket chains, and private-label brand owners face an increasingly sophisticated market. At the epicenter of this industrial evolution lies China’s export manufacturing hub—a global powerhouse capable of producing high-volume, highly technical, and eco-conscious cat litter formulations.
When evaluating China top export litter factories & factory networks, enterprise procurement officers must look beyond simple FOB price quotes. True competitive advantage stems from holistic manufacturing capabilities: raw material vertical integration, ultra-low dust screening engineering, rapid clumping formulation, bio-degradable material science, and customized high-speed packaging automation.
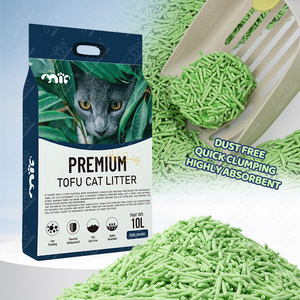
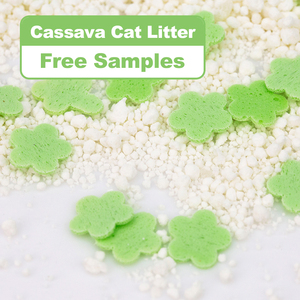
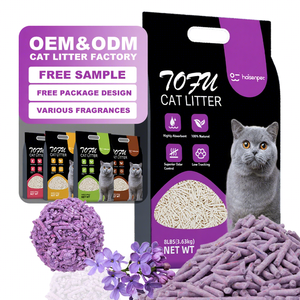
Modern pet owners demand cat litter that bridges the gap between hygiene performance and environmental responsibility. From natural plant-based substrates like pea fibre, soybean curd (tofu), corn starch, and cassava starch, to mined mineral reserves such as premium white calcium bentonite, leading Chinese factories have established integrated supply networks that guarantee lot-to-lot consistency, stable moisture levels, and zero harmful synthetic additives.
Key technological innovations and consumer shifts reshaping international cat litter sourcing strategy.
Understanding where the cat litter market is heading is critical for global distributors and brand managers planning multi-year procurement contracts. Based on trade volume analysis and consumer feedback across major retail channels, four key macroeconomic and technical trends are reshaping factory production lines:
Consumer shift away from non-renewable silica and heavy clay toward 100% flushable cassava and soybean tofu litter. High-absorption pea fiber blends are projected to capture 40% of premium European and Asian retail shelf space by 2028 due to urban waste-disposal convenience.
Feline respiratory health and home dust elimination have become non-negotiable buyer demands. Leading export factories utilize multi-cyclone dust extraction systems, reducing airborne particulate matter down to <0.5%, yielding a 99.5% dust-free standard.
Surface fragrancing is being replaced by molecular odor locking. Importers are prioritizing formulations integrated with micro-porous activated carbon, STA odor-eliminating beads, and natural enzymes that neutralize ammonia instantly upon liquid contact.
To assist procurement managers in choosing the right product mix for their target demographic, the table below outlines technical specifications across major China-manufactured cat litter types:
| Substrate Category | Primary Raw Material | Clumping Speed | Absorption Ratio | Dust Rating | Disposal Method | Ideal Target Market |
|---|---|---|---|---|---|---|
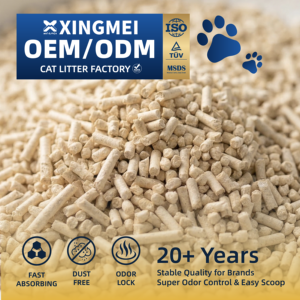
| Tofu Pellets (2.0mm / 1.5mm) | Food-grade Pea Fiber & Soybean | < 3 Seconds | 300% - 400% | 99.5% Dust Free | Toilet Flushable / Compostable | Urban Apartments, Eco Brand Lines |
| Cassava Granules | Natural Cassava Tapioca Starch | < 2 Seconds | 400% - 500% | 99.2% Dust Free | Toilet Flushable / Biodegradable | Ultra-Premium Private Label, Low-Tracking |
| White Calcium Bentonite | Natural Montmorillonite Clay Reserve | < 5 Seconds | 220% - 280% | 99.0% Dust Free | Landfill / Standard Waste | Mass Market Retail, Supermarket Chains |
| Mixed Hybrid (Tofu + Bentonite) | 70% Tofu + 30% Mineral Granules | < 2.5 Seconds | 350% | 99.3% Dust Free | Standard Waste / Partial Flush | Multi-Cat Households, Odor Control Focus |
Combining mineral asset ownership with cutting-edge plant processing and international certification compliance.
Selecting a manufacturing partner requires verifying end-to-end supply chain control. Our production ecosystem integrates raw material extraction, continuous R&D formulation, automated dust sieving, high-speed vacuum sealing, and container loading under one unified ISO 9001 and ISO 14001 certified management standard.
Whether processing natural Montmorillonite white bentonite clay directly from licensed reserves or sourcing non-GMO food-grade pea fibers for plant-based manufacturing, our raw material inputs undergo strict moisture and purity testing prior to processing. This eliminates seasonal variation in clumping performance.
We serve global distributors, retail supermarket chains, and direct-to-consumer e-commerce brands with complete custom packaging solutions. From 5L and 10L vacuum bags with heavy-duty handles to rigid bucket packaging, custom box configurations, and big-bag bulk packaging (1,000kg to 1,250kg), our automated packing lines ensure rapid order fulfillment and precise net-weight calibration.
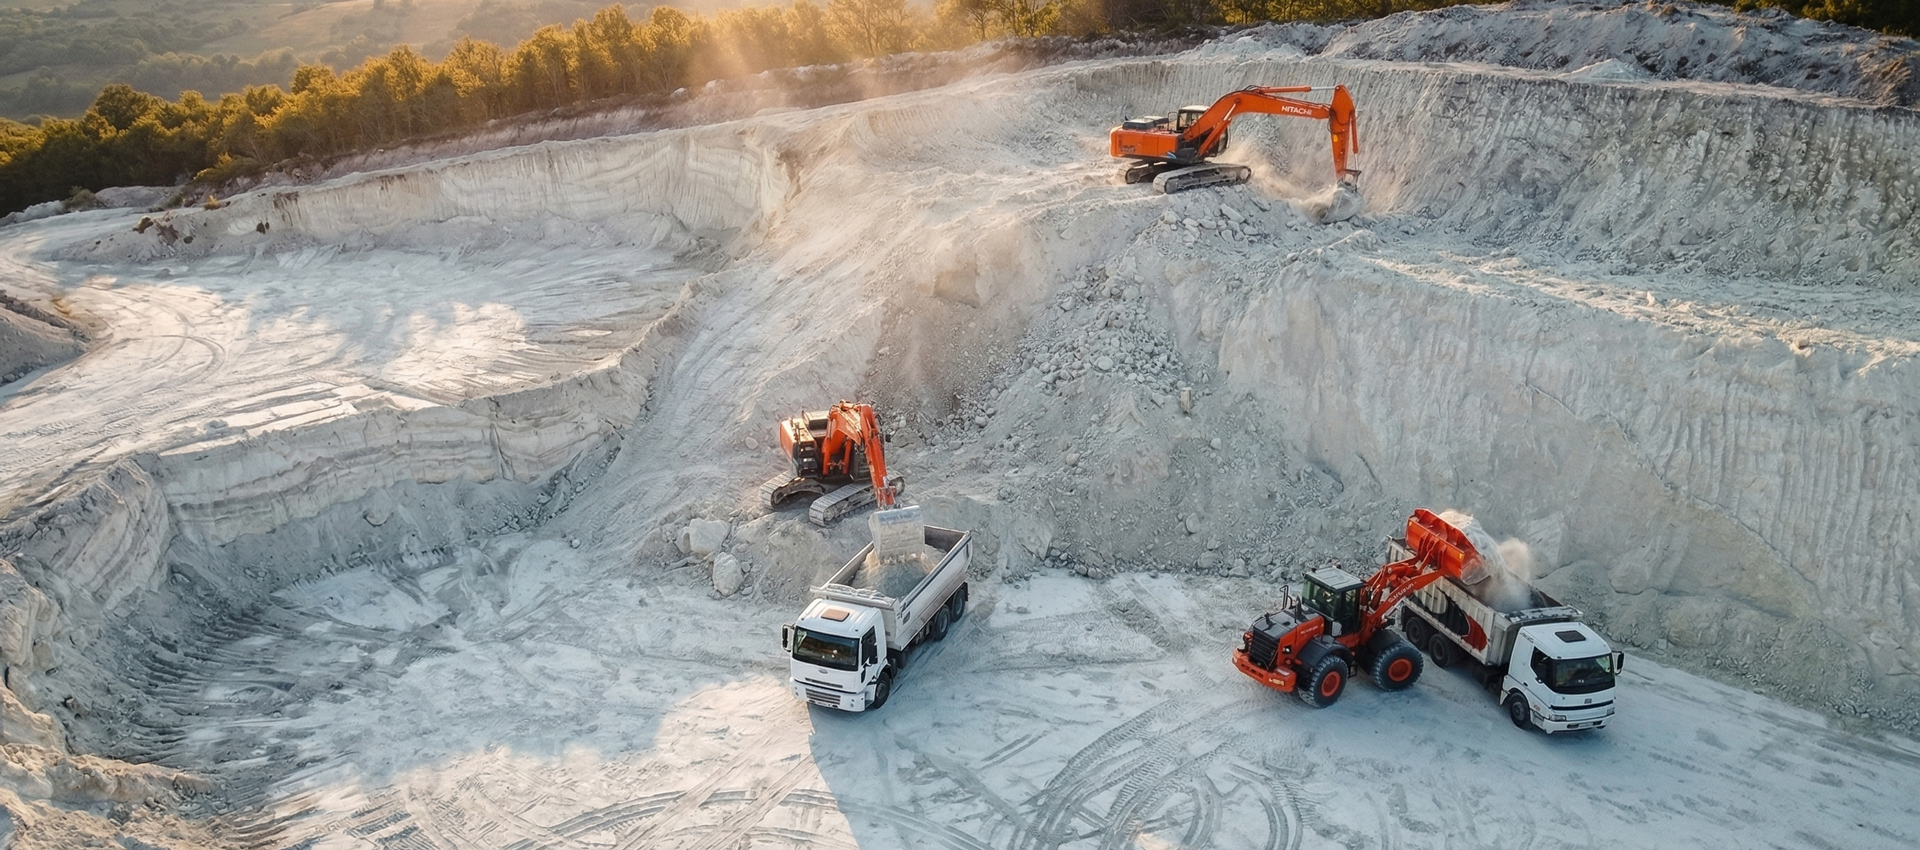
Owned raw material reserves guarantee stable supply, zero iron contamination, and consistent white granule aesthetics.
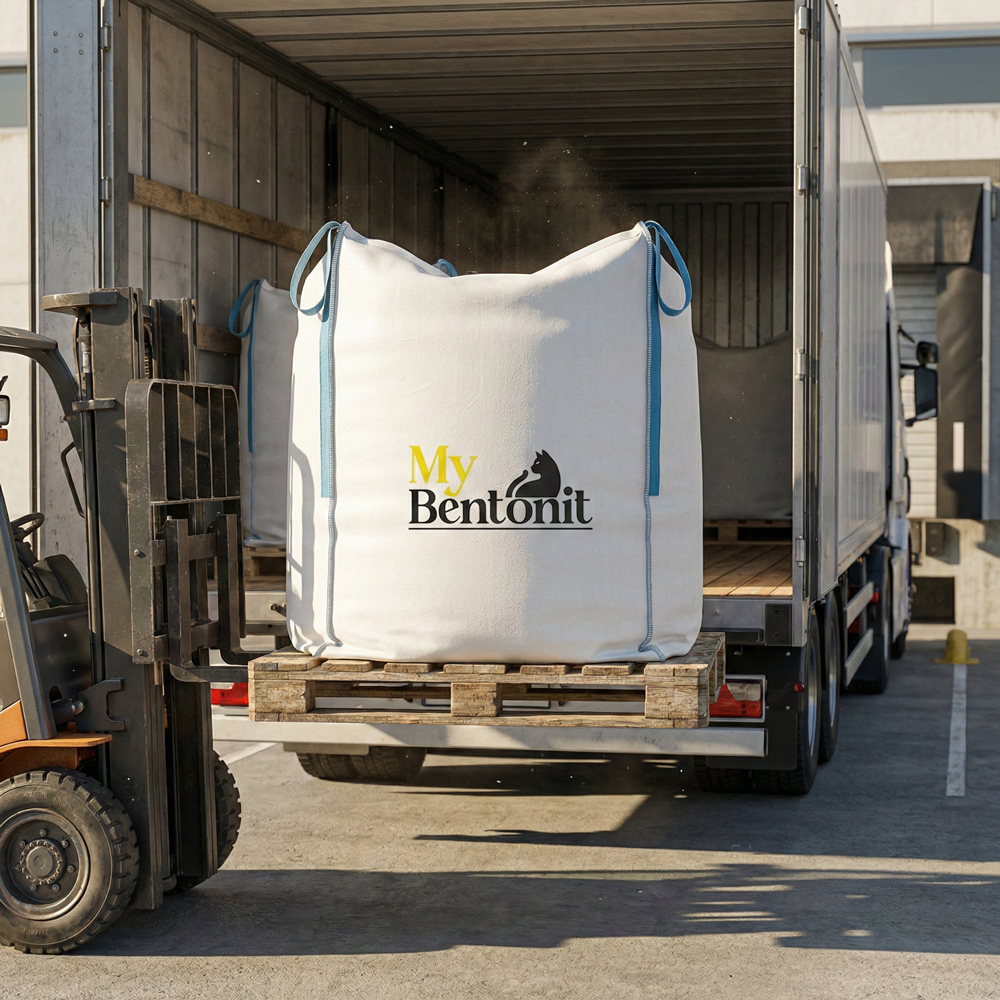
1,000kg–1,250kg ton bags for overseas repackers and large-scale industrial pet food distributor operations.
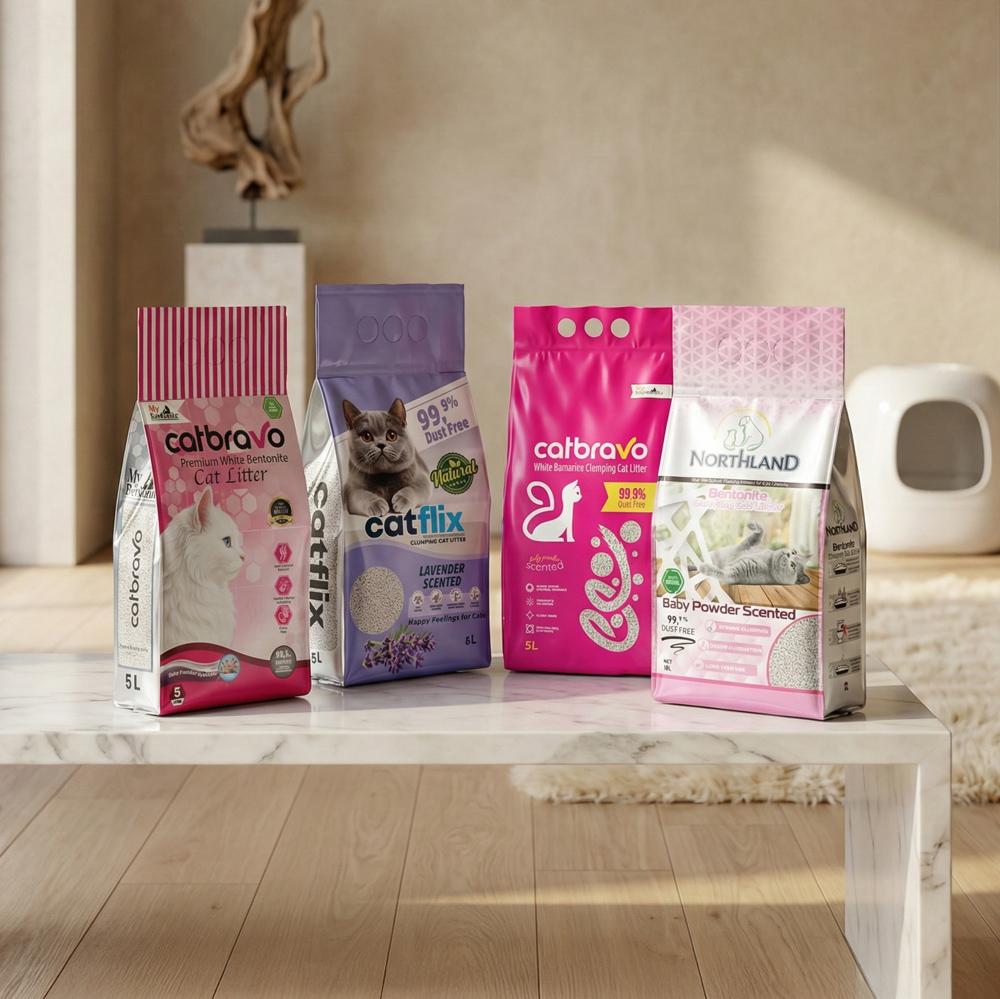
Fully automated vacuum sealing, handle bag integration, and shrink-wrapped palletization for safe sea freight transit.
Addressing essential technical, logistical, and OEM questions asked during contract negotiations.
Partner directly with top-tier China export factories. Request technical spec sheets, order custom sample kits, or initiate private-label discussions today.
Contact Us