Explore our complete range of processed mineral granules mined, dried, sieved, and packaged under rigid ISO 9001 and CE quality management standards.
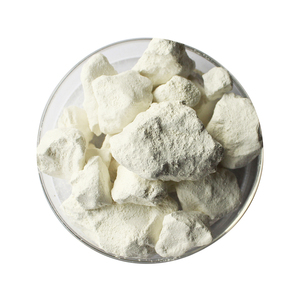 Ceramic & Paper Grade
Refined high-whiteness washed kaolin granules offering exceptional refractory index, low iron impurities, and optimal opacity control.
 Agri & Carrier Grade
Natural high-swelling calcium bentonita granules designed as nutrient carriers, soil conditioners, and eco-friendly fertilizer granulating bases.
 Filtration & Refining
Acid-activated granular bleaching clay delivering superior decolorization efficiency and heavy metal adsorption for edible oils and fats.
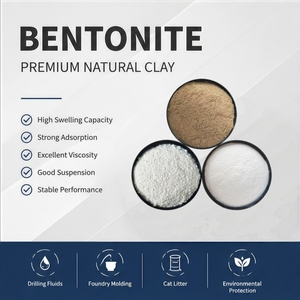 Paint & Coatings
Multi-mesh size natural white bentonite providing high-performance anti-settling, thickening, and thixotropic stability in solvent and waterborne systems.
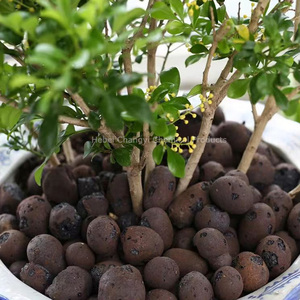 LECA Aggregate
Lightweight expanded clay aggregate (LECA) calcined at 1200°C for hydro-culture, drainage control, and structural lightweight concrete applications.
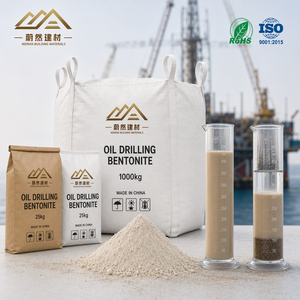 Drilling & Civil
High-yield drilling mud bentonite granules with instant hydration characteristics engineered for mineral exploration, core sampling, and trenching.
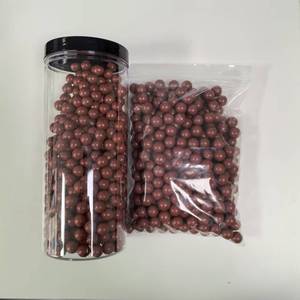 Precision Molded
Eco-friendly, 100% biodegradable compressed clay pellets engineered for high-accuracy target practice, custom colors, and zero environmental residual impact.
 99% Pure Mineral
Pharmaceutical and industrial grade ultra-white montmorillonite clay featuring exceptional cation exchange capacity and superior thixotropic control.
From our vast white calcium bentonite reserves in Fatsa, Ordu (Türkiye) to specialized multi-stage screening facilities, we eliminate intermediaries to guarantee batch consistency and direct cost efficiency.
We own and operate our primary mineral reserves in Fatsa, Ordu. Every lot of calcium bentonite and kaolin can be traced directly back to the extraction bench, ensuring uniform chemical profiles and zero contamination risk.
Our manufacturing and processing lines strictly comply with ISO 9001:2015 standards and CE regulatory directives for industrial construction, drilling additives, and environmental containment solutions.
Utilizing high-efficiency rotary screen separators and multi-stage air-cyclone de-dusting circuits, our clay granules achieve up to 99.5% dust-free purity, optimizing workplace safety and mechanical performance.
A comprehensive technical evaluation matrix designed for chemical engineers, procurement officers, and industrial R&D teams selecting optimal clay granule matrices.
| Granule Type | Primary Mineral Base | Montmorillonite / Kaolinite % | Swelling Capacity | Cation Exchange (CEC) | Thermal Stability Limit | Key Industrial Benchmark |
|---|---|---|---|---|---|---|
| Natural Calcium Bentonite | Calcium Smectite | 80% – 85% | 8 – 14 ml/2g | 75 – 90 meq/100g | Up to 750°C | High Bio-Absorbency |
| Sodium-Activated Bentonite | Modified Sodium Smectite | 85% – 92% | 24 – 36 ml/2g | 90 – 110 meq/100g | Up to 850°C | Rapid Hydration Yield |
| 99% Pure Montmorillonite | Ultra-Refined Smectite | ≥ 99% | 30 – 40 ml/2g | 100 – 120 meq/100g | Up to 900°C | Pharmaceutical / Rheology |
| Acid-Activated Bleaching Earth | Leached Smectite Structure | 70% – 80% | Non-Swelling | 40 – 60 meq/100g | Up to 500°C | Adsorption & Color Removal |
| Washed Paper & Ceramic Kaolin | Hydrous Aluminum Silicate | ≥ 88% Kaolinite | Negligible | 5 – 15 meq/100g | Up to 1650°C (Refractory) | High Whiteness & Opacity |
| Calcined LECA Ceramsite | Expanded Sintered Clay | Vitreous Matrix | 0% (Inert) | Near Zero | Up to 1200°C | Structural Aggregate |
For B2B buyers in civil engineering, oil purification, and agricultural carrier industries, Cation Exchange Capacity (CEC) serves as the definitive benchmark of active mineral performance. The high montmorillonite content present in our Fatsa-extracted calcium white bentonite grants an extraordinary CEC ratio between 75 and 120 meq/100g. This molecular structure enables rapid exchange of calcium, magnesium, and sodium cations, directly driving fluid absorption rates, clump formation hardness, and heavy-metal binder efficiency.
When selecting clay granules, understanding particle size distribution (PSD) curves is equally critical. Oversized granules reduce active surface area, while micro-fine dust creates handling hazards and filter blockages. Our proprietary multi-deck vibration screening ensures strict compliance with customized sieve fractions (e.g., 0.5–1.5mm fine mesh, 1.0–3.0mm standard classic, and 2.0–5.0mm low-tracking coarse granules).
Macro-economic factors, environmental legislation, and technological innovations are reshaping how international buyers audit and procure industrial clay minerals.
European and North American buyers are increasingly enforcing strict Scope-3 carbon limits across imported raw materials. Manufacturers operating integrated mine-to-plant setups—utilizing solar drying yards and low-emission calcination kilns—offer a measurable carbon advantage over third-party repackers who transport raw ores across long domestic distances before processing.
Global shipping disruptions have exposed the vulnerabilities of multi-tiered chemical supply chains. Procuring CE-certified clay granules directly from primary mine operators in strategic logistical hubs like Türkiye (bordering Europe, Asia, and the Middle East) drastically shortens transit lead times and protects pricing against broker speculation.
Industrial health and safety agencies (OSHA, EU-OSHA) have tightened indoor airborne silica and mineral dust exposure standards. Modern procurement mandates require dust-free thresholds of ≥ 99.5%. Processing lines equipped with vacuum-cyclone dedusting and electrostatic dust collectors have shifted from a luxury feature to a mandatory procurement specification.
Industrial applications are shifting from raw mineral usage toward tailored organoclay formulations. Buyers now demand clay granules functionalized with bio-based surfactants, activated carbon cores, or antimicrobial ions for high-value uses ranging from environmental spill remediation to specialized animal nutrition carriers.
Continuous innovation in thermal treatment, automated particle size classification, and eco-friendly granulation binding systems.
Traditional thermal activation consumes massive amounts of energy. Next-generation processing utilizes targeted chemical activation combined with low-temperature fluid-bed dryers, reducing carbon intensity while optimizing swelling yield and CEC capabilities.
Integrating high-speed optical camera sorters directly onto granule conveyor belts allows automated removal of off-color minerals and impurities. This technology guarantees standard whiteness levels above 88% ISO for premium ceramic and paper filler grades.
Modern processing lines now seamlessly transition from 1,000kg industrial Big Bags to retail-ready 5L–20L printed bags. Integrated robotic palletizers and moisture-barrier stretch hoods protect product integrity during long-distance transoceanic transit.
Direct technical answers to common inquiries from international purchasing directors, chemical distributors, and OEM buyers.
Every shipment is backed by a comprehensive Technical Data Sheet (TDS), Certificate of Analysis (COA) per lot, Material Safety Data Sheet (MSDS), and relevant CE compliance documentation for industrial and civil engineering usage. Factory audits can be arranged upon request.
White calcium bentonite extracted from our Fatsa reserves exhibits naturally high montmorillonite purity, low iron oxide content, and superior visual cleanliness. Unlike dark grey sodium bentonite, white granules provide high liquid pick-up without leaving muddy residue or unappealing dark dust footprints, making it ideal for premium absorption products and sensitive carrier matrices.
We offer flexible bulk logistics including 1,000 kg to 1,250 kg UV-stabilized Big Bags (Jumbo Bags) with discharge spouts, as well as valve-sealed 25 kg paper/PE sacks. Packed goods are palletized, corner-protected, and stretch-wrapped. Standard 20-foot sea containers fit up to 24–25 metric tons depending on granule density.
Yes. Our multi-deck vibrating screen systems allow us to engineer custom particle size distributions (PSD) ranging from 0.5 mm up to 5.0 mm, or fine powders down to 325 mesh. Moisture levels are strictly controlled between 6% and 10% depending on your moisture-sensitivity requirements.
Standard industrial trial samples (1 kg – 5 kg) can be dispatched via international express within 48 hours alongside official TDS documentation. Full container production orders typically ship within 10 to 14 business days from contract confirmation and deposit approval.
Yes. Our full-service private label program covers artwork adaptation, multi-color printed PE bags, handle bags, box packaging, barcode application, and pallet configuration tailored specifically to your regional retail market requirements.
Request technical specification sheets, schedule a factory audit, or obtain competitive FOB/CIF container price quotes directly from our sales engineering team.